


In the first issue of the article, the author concluded through analysis that the internal stress of injection molding is the ultimate killer of the electroplating properties of materials. Improving the electroplating properties of materials through the injection molding process means that the internal stress in the molding process needs to be improved. At the same time, in the second issue of the article, we analyzed the improvement direction of the material's electroplating performance from the temperature aspect, which attracted everyone's attention. Many readers asked whether there are other ways? Today, we mainly analyze how to improve the residual stress of the material and further improve the electroplating performance of the material from the pressure and speed parameters of the injection molding process.
The pressure effect is mainly the injection pressure in the injection stage and the holding pressure in the holding pressure stage, and the screw back pressure in the melting stage has a smaller effect. In general, low injection pressure and low holding pressure are beneficial to improve the internal stress of the molding and improve the electroplating performance of the material.
In the injection molding stage, if the injection pressure is too high, the internal molecular orientation of the product will be serious in the mold cavity, which will cause the product to have unrelaxed high elastic deformation after cooling, and then generate orientation stress, which will lead to poor electroplating bonding force of the product. problem. The orientation stress produced by high-pressure injection is mainly concentrated on the surface of the product and the vicinity of the gate.
In the holding pressure stage, the high holding pressure will increase the injection stress of the product. A considerable part of the total deformation of the cooling melt under the action of external pressure is elastic, and the melt will condense under high pressure. Large internal stress and polymer orientation are generated in the parts. Pressure reduction immediately after compaction or the use of segmented pressure retention (stepwise pressure reduction during the refilling process) is conducive to the de-orientation of the polymer, so reducing the pressure and shortening the pressure time is beneficial to the reduction of the orientation stress and the improvement of the material Electroplating performance; and the impact of high holding pressure on the stress between products is mainly concentrated in the gate position of the product.
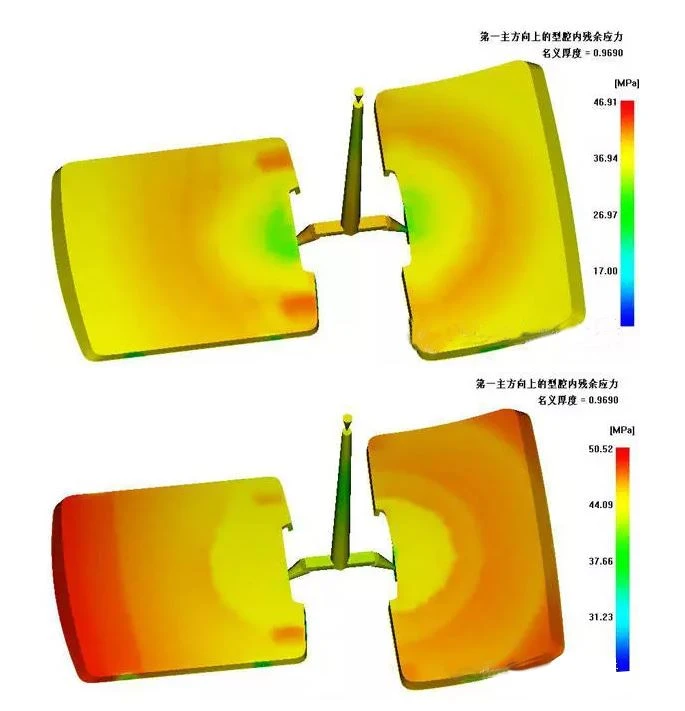
The picture shows the mold flow analysis pictures of high injection pressure/high packing pressure and low injection pressure/low packing pressure respectively.
In the melting stage, adopting proper back pressure control is conducive to the plasticization of the material in the screw, thereby improving the fluidity of the material, reducing the resistance during the filling process, and also appropriately reducing the internal stress of the molding, which can improve the electroplating of the material. The effect of performance; but in general, the screw back pressure has little effect on the internal stress of the molding, mainly to improve the plasticization and exhaust.
Speed effect
During the molding process, there are three speed parameters that can be set, namely: injection speed, pressure holding speed, and screw speed.
Injection speed: For general materials, the effect of injection speed on the electroplating performance of the material is divided into two opposite directions. When the injection speed is increased, the degree of orientation of the material through the gate position increases, resulting in an increase in the orientation internal stress, which is a bad side compared to improving the electroplating performance of the material. However, when the injection speed is increased, the shear heat generated when the material passes through the gate position will also increase. The shear heat will increase the actual temperature of the material, thereby improving the fluidity of the material and reducing the internal stress. For improving the electroplating performance of the material, This is another advantage; therefore, for general-purpose materials, when adjusting the electroplating performance of the material through the injection speed, it is mainly to see which influence is dominant; for the electroplated ABS material, related experiments show that the influence of the material orientation caused by high-speed injection Occupy the leading role. Under the condition of high-speed injection, the rubber particles in the material produce tensile deformation, resulting in uneven roughening and etching, which affects the electroplating performance of the material; the test proves (as shown in the figure below) that high-speed injection will make the material ABS material The reduction of electroplating bonding force, which in turn affects the overall electroplating performance.

Pressure holding speed: The holding pressure stage is mainly controlled by pressure and time. The holding pressure speed is generally low speed, so the holding pressure speed basically does not affect the electroplating performance of the material.
Screw speed: The screw speed will affect the uniformity of plasticization. Too fast screw speed will cause the mixing effect of the plastic to deteriorate, and the melt temperature will be uneven, which will cause differences in filling flow and cooling, which is also caused by the internal stress of the product. One of the reasons is that at this time, the electroplating performance of the material will be reduced. Therefore, generally speaking, under the premise of ensuring the melting of the material, the screw speed is set so that the melt metering is completed before the end of cooling.
Generally speaking, in the injection molding process, low injection pressure and low holding pressure are beneficial to reduce the internal stress of the material, thereby improving the electroplating performance of the material. The effect of injection speed on the electroplating performance of the material should be treated differently, find its dominant direction, and then prescribe the right medicine.


